INDUSTRIAL PRODUCT
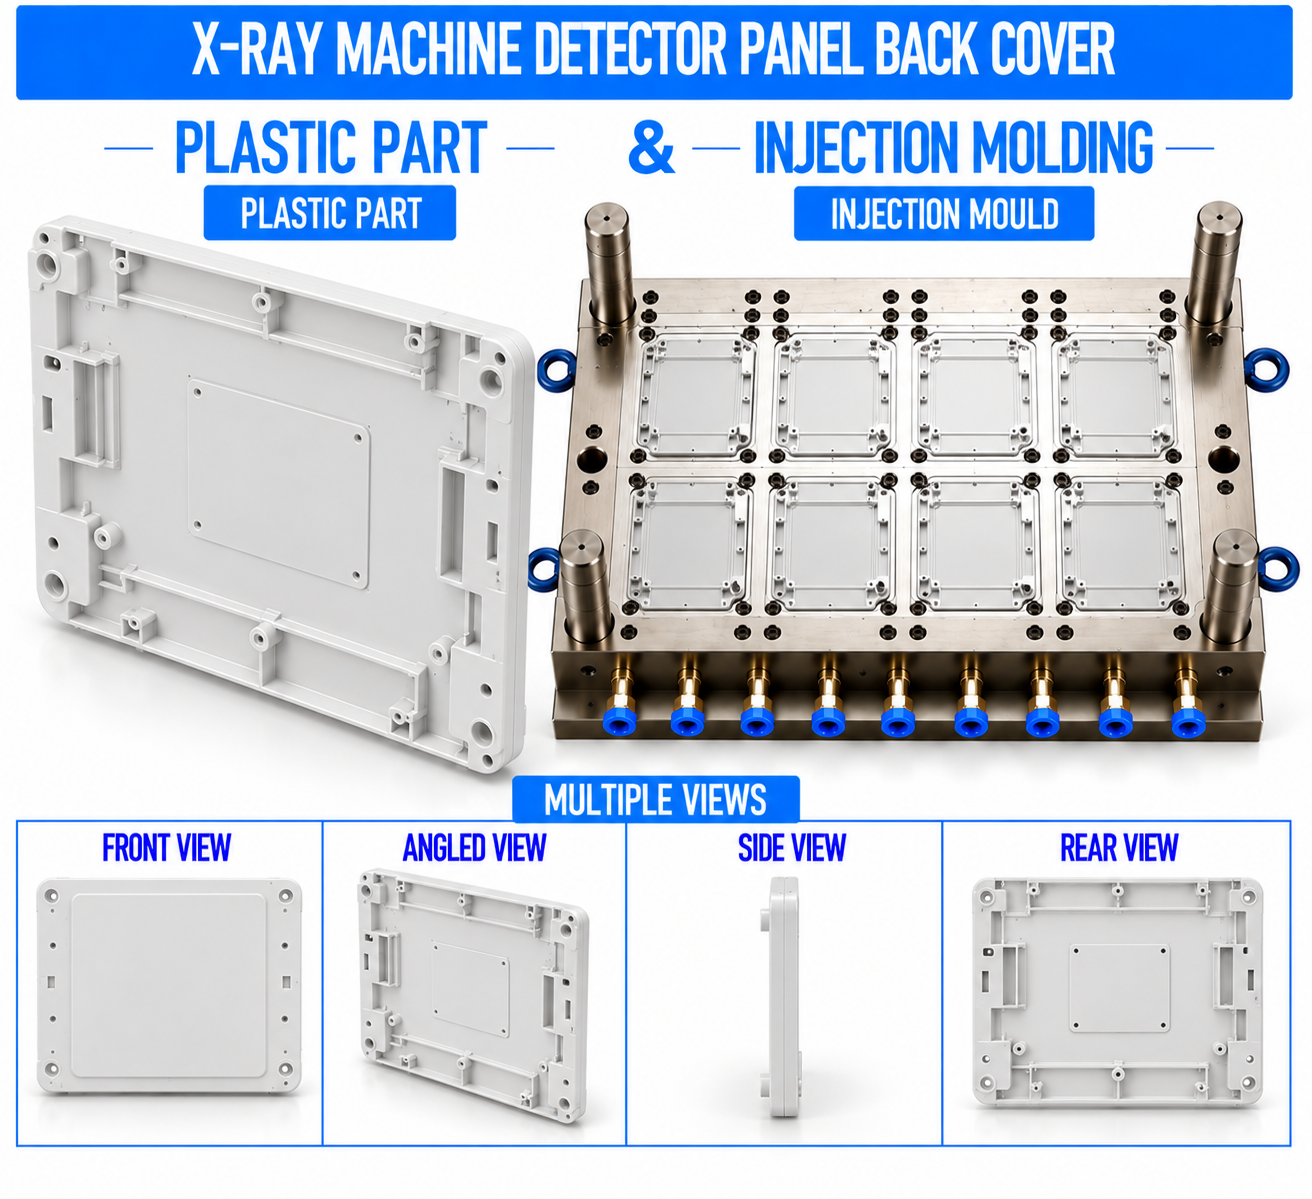
X-Ray Machine Plastic Detector Panel Back Cover Mould and Moulding Service
₹800.00
X-Ray Machine Plastic Detector Panel Back Cover Mould and Moulding Service | Renovator Appliances Ltd
Product Overview
Renovator Appliances Ltd manufactures X-Ray Machine Plastic Detector Panel Back Covers using precision Plastic Injection Moulding and customized mould manufacturing processes. The detector panel back cover is the rear enclosure component of an X-ray detector panel assembly. It protects internal electronic and structural components while providing mounting interfaces, cable-routing provisions, ventilation features, service access, and integration with the front cover.
The back cover is designed according to the complete detector panel architecture, including internal electronics, detector modules, batteries where applicable, communication connectors, cable routing, mounting points, heat-management requirements, and front-cover mating geometry. Accurate injection moulding helps maintain dimensional stability, panel alignment, and reliable assembly.
Customized features such as connector openings, cable passages, ventilation slots, screw bosses, locating ribs, snap-fits, battery-access covers, handles, mounting interfaces, and service openings can be incorporated according to the detector design.
The plastic back cover should not be assumed to provide radiation shielding unless its material, thickness, geometry, and complete assembly have been specifically engineered, tested, and validated for that purpose.
Key Features
Precision moulded detector-panel back cover
Customized rear enclosure profile
Accurate front-to-back housing mating interface
Internal electronic-component clearance
Connector and cable-routing openings
Ventilation and heat-management provisions where required
Reinforced mounting bosses
Locating ribs and alignment features
Controlled wall thickness
Screw-fit, clip-fit, or snap-fit options
Service-access provisions
Smooth and consistent exterior surface
Lightweight structural construction
Suitable for OEM and ODM production
Industrial Applications
| Application Area | Component Function |
|---|---|
| X-Ray Detector Panel | Forms the protective rear enclosure |
| Digital Radiography Equipment | Protects internal detector electronics and assemblies |
| Portable X-Ray Detector | Provides a lightweight rear housing component |
| Fixed X-Ray Systems | Integrates the detector assembly with surrounding equipment |
| Medical Imaging Equipment | Provides rear structural and protective enclosure |
| OEM X-Ray Equipment | Customized back cover according to detector-panel design |
Manufacturing Process
1. Product Design & Development
The back cover is developed according to the complete detector panel assembly. Important parameters include overall panel dimensions, rear profile, internal component clearance, connector locations, cable routing, ventilation requirements, mounting points, battery access where applicable, and the mating interface with the front cover.
Special attention is given to wall thickness, ribs, bosses, and large flat surfaces to achieve adequate structural rigidity while controlling shrinkage and warpage.
2. Plastic Mould Design
The injection mould is designed to accurately reproduce the rear-cover profile, mounting bosses, locating ribs, connector openings, cable passages, ventilation slots, service features, and front-cover mating surfaces.
Parting-line placement, gate location, draft angles, ejector arrangement, cooling channels, and shrinkage allowance are optimized for the component geometry. Large rear-panel areas are designed to reduce warpage, sink marks, flow marks, and dimensional variation.
3. Mould Manufacturing
The mould is manufactured using precision machining, EDM, polishing, fitting, and mould assembly processes. P20, H13, S136, or another suitable mould steel can be selected according to production quantity, plastic material, surface-finish requirements, and expected mould life.
Critical cavity dimensions, mounting features, connector openings, and mating surfaces are inspected before production trials.
4. Injection Moulding
The selected plastic material is injection moulded under controlled processing conditions. Injection pressure, speed, melt temperature, holding pressure, cooling time, and cycle parameters are adjusted according to the selected material and back-cover geometry.
Controlled processing helps maintain panel flatness, mounting accuracy, opening dimensions, surface quality, and consistent fitment with the detector front cover.
5. Finishing & Assembly Preparation
After moulding, gates, runners, flash, and excess material are removed. Connector openings, cable passages, ventilation slots, mounting holes, bosses, locating features, and service-access areas are checked for obstruction or moulding defects.
Where required, the back cover can be prepared for labels, markings, protective components, battery-access features, handles, connectors, or other assembly operations.
6. Quality Inspection
Finished back covers are inspected for overall dimensions, panel flatness, front-cover mating geometry, mounting-hole positions, connector openings, cable passages, ventilation features, internal clearances, wall thickness, warpage, surface finish, and flash.
Trial assembly with the detector panel, front cover, internal electronics, and associated components can be performed to verify mechanical fit and alignment.
Raw Materials
| Material / Component | Typical Selection Consideration |
|---|---|
| ABS | Suitable for rigid detector housing applications requiring good surface appearance |
| PC+ABS | Considered where improved impact resistance and dimensional stability are required |
| PC | Suitable where higher impact performance and dimensional stability are required |
| PBT | Considered where dimensional stability and mechanical performance are important |
| Flame-Retardant ABS | Used where specified flame-retardant properties are required |
| Flame-Retardant PC+ABS | Considered where specified flame-retardant and mechanical properties are required |
| Engineering Plastic | Selected according to mechanical, thermal, dimensional, and equipment requirements |
| P20 Steel | Suitable for general-purpose production moulds |
| H13 Steel | Suitable for demanding production conditions |
| S136 Steel | Suitable where corrosion resistance and high-quality mould surfaces are required |
Material selection should consider impact resistance, detector operating temperature, dimensional stability, electrical requirements, surface finish, environmental exposure, and applicable medical-equipment specifications.
Quality Control
Renovator Appliances Ltd focuses on the following quality parameters during production:
Overall back-cover dimensions
Panel flatness
Front-to-back housing fitment
Mounting-hole position
Mounting-boss dimensions
Locating-feature accuracy
Connector opening dimensions
Cable-entry and routing clearance
Ventilation-opening accuracy
Internal electronic-component clearance
Wall thickness consistency
Rib and reinforcement dimensions
Screw-fit or snap-fit accuracy
Service-access opening dimensions
Warpage inspection
Sink-mark inspection
Flash and burr inspection
Surface-finish inspection
Colour consistency
Assembly alignment
Material-grade verification
Batch-to-batch dimensional consistency
Buyer Guide
Before ordering an X-Ray Machine Plastic Detector Panel Back Cover Mould and Moulding Service, buyers should provide:
Detector panel CAD drawing or sample
Complete back-cover dimensions
Front-cover mating dimensions
Internal component arrangement
PCB and electronic-component dimensions
Connector locations
Cable-routing requirements
Ventilation requirements
Battery-access requirements where applicable
Mounting-hole and fastening details
Required ribs and reinforcement
Plastic material specification
Colour and surface-finish requirements
Expected production quantity
Required mould life
Prototype requirements
Providing the complete detector panel assembly helps establish accurate front-to-back housing alignment, connector positioning, internal clearances, mounting interfaces, and service-access requirements.
The plastic back cover should not be treated as a radiation-shielding component unless its material, thickness, geometry, and complete assembly have been specifically engineered and validated for that function. Final medical-equipment validation should address applicable mechanical, electrical, thermal, imaging, radiation-safety, and regulatory requirements.
Why Choose Renovator Appliances Ltd?
Advanced Injection Moulding Facility
Renovator Appliances Ltd supports precision Plastic Injection Moulding for detector-panel back covers requiring controlled dimensions, flatness, detailed openings, and reliable assembly fitment.
In-House Mould Manufacturing
In-house mould manufacturing supports customized rear-panel profiles, mounting bosses, ribs, connector openings, ventilation features, cable passages, and service-access details.
OEM & ODM Manufacturing
Customized detector-panel back covers can be manufactured according to customer CAD drawings, samples, detector specifications, and complete equipment designs.
Quality Assurance
Dimensional inspection, flatness checks, opening verification, mounting-feature inspection, surface inspection, and trial assembly help maintain consistent back-cover quality.
Cost-Effective Manufacturing
Mould design, material selection, injection parameters, and production configuration can be optimized according to component complexity and production volume for efficient manufacturing.
Frequently Asked Questions
1. What is an X-Ray Machine Plastic Detector Panel Back Cover?
It is a moulded plastic rear enclosure component that protects and supports the internal components of an X-ray detector panel while providing mounting, cable, connector, ventilation, and housing-interface features.
2. Can the back cover include connector and cable openings?
Yes. Connector cut-outs, cable passages, cable-routing features, ventilation openings, service openings, and other customized interfaces can be incorporated into the mould.
3. Can the back cover be designed with mounting bosses and ribs?
Yes. Screw bosses, locating ribs, reinforcement structures, snap-fits, clips, and other assembly features can be integrated according to the detector-panel design.
4. Does the plastic back cover provide radiation shielding?
Not automatically. Radiation shielding should only be claimed when the complete material construction and assembly have been specifically engineered, tested, and validated for that purpose.
5. Can Renovator Appliances Ltd manufacture both the back-cover mould and moulded parts?
Yes. Renovator Appliances Ltd supports component development, mould design, mould manufacturing, Plastic Injection Moulding, quality inspection, prototype production, and bulk OEM/ODM manufacturing.
- SKU
- REN-16AFB3216C8FF76470EDC850